
Stainless Steel for Prototypes: Grades, Machining & Applications
Need stainless steel prototype parts for design validation, functional testing or low volume production? Learn how to select the right grade, choose a manufacturing process, specify tolerances and control prototype costs with support from Manufyn’s Indian manufacturing network.
Request a Prototype RFQ → Compare Steel Grades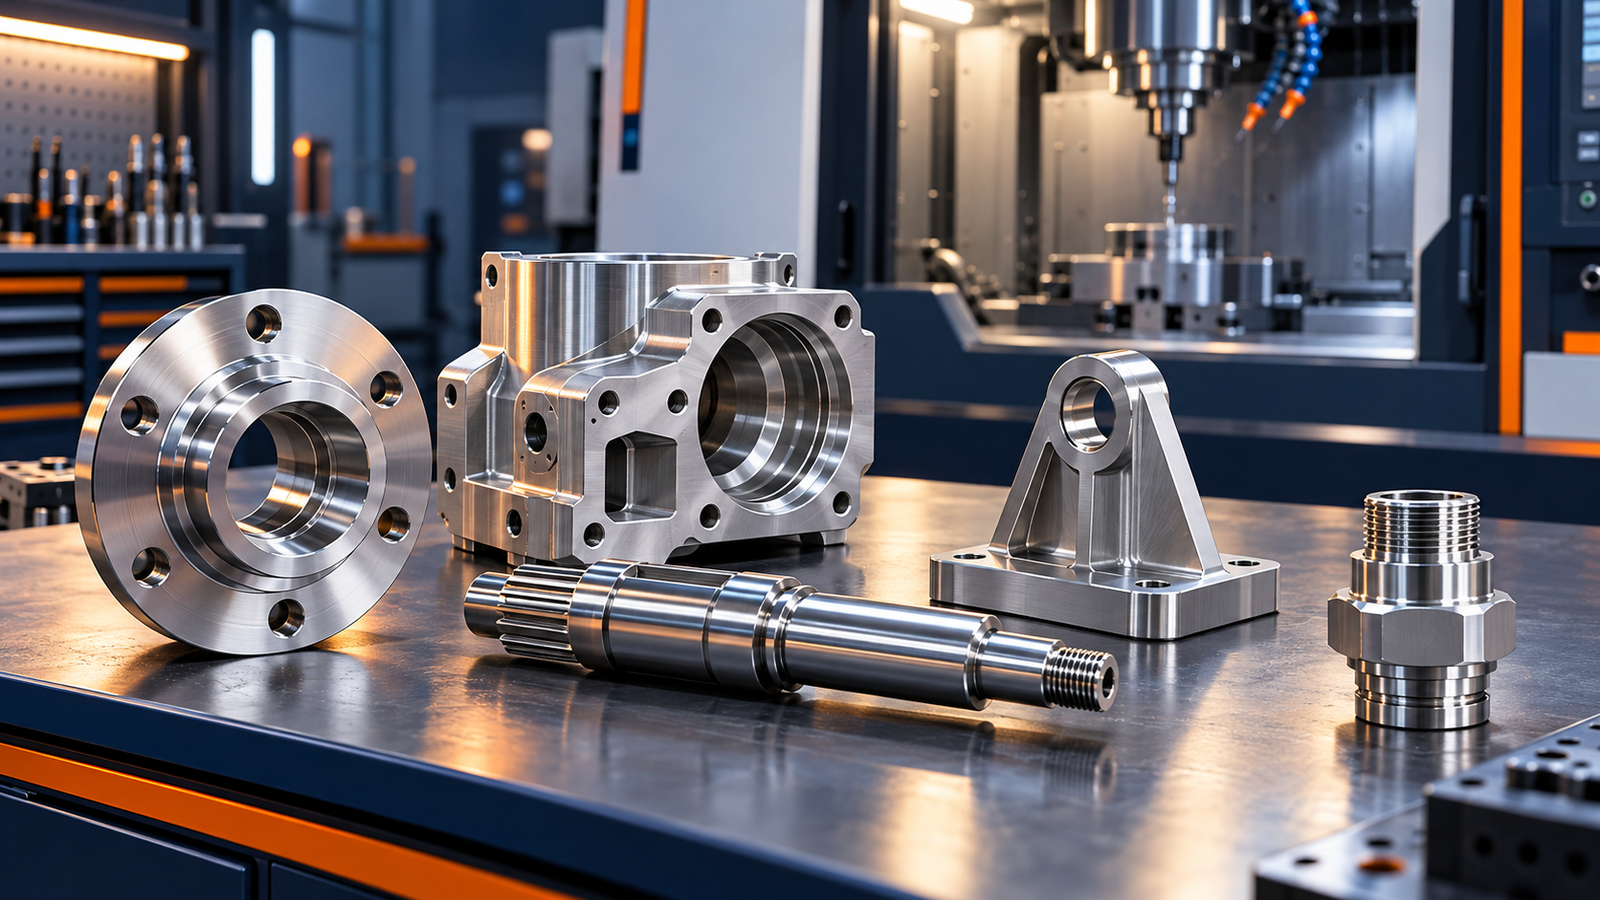
What Is Stainless Steel for Prototypes?
Stainless steel prototyping is the process of manufacturing sample components from stainless steel to evaluate a product’s fit, function, durability and manufacturability before production. These prototype parts can be used to test assemblies, validate mechanical interfaces, evaluate corrosion resistance or confirm a design under realistic operating conditions.
Stainless steel is an iron based alloy containing chromium, which helps form a protective passive surface layer. Different grades offer different combinations of corrosion resistance, strength, machinability, weldability and temperature performance. The correct selection depends on the environment and intended function of the part.
Which Stainless Steel Grade Is Best for Prototype Parts?
Select a stainless steel grade based on corrosion exposure, loading, temperature, machining complexity, finishing requirements and the production material specification. The following grades are common starting points for engineering discussions.
| Grade | Key characteristics | Typical prototype applications | Selection consideration |
|---|---|---|---|
| 303 | Free machining austenitic stainless steel | Turned shafts, bushings, fittings and precision features | Useful when machinability is important; corrosion resistance and weldability differ from 304. |
| 304 / 304L | Versatile austenitic grade with good general corrosion resistance | Brackets, housings, enclosures and general industrial components | A common starting point for general purpose prototypes. 304L has lower carbon content. |
| 316 / 316L | Improved resistance in many chloride containing and corrosive environments | Marine hardware, fluid handling parts and selected medical or process equipment prototypes | Assess the actual chemical exposure; 316 is not resistant to every corrosive environment. |
| 17-4 PH | Precipitation hardening stainless steel with high strength potential | Load bearing fixtures, shafts, robotics components and demanding functional parts | Specify the required heat treatment condition and final mechanical properties. |
| 310 / 310S | Designed for elevated temperature service | Heat exposed components and thermal equipment prototypes | Confirm actual operating temperature, atmosphere and required mechanical properties. |
| Duplex 2205 | High strength and strong resistance to many corrosive environments | Selected chemical processing, marine and demanding fluid handling components | Machining and material availability need to be assessed for the particular design. |
These are general material selection guidelines, not substitutes for an engineering specification. Confirm the applicable material standard, condition, certification and required properties before placing an order.
Manufacturing Processes for Stainless Steel Prototypes
The best process depends on part geometry, required surface finish, dimensional tolerances, quantity and whether the prototype must replicate a production process.
CNC Machining
Suitable for complex metal parts, machined housings, mounting brackets, pockets, slots and precision interfaces. CNC milling removes material from a solid workpiece.
CNC Turning
Ideal for rotational parts such as shafts, sleeves, bushings, threaded fittings and cylindrical components. Live tooling can support selected additional features.
Sheet Metal Fabrication
Appropriate for enclosures, covers, brackets and formed components. The design may require laser cutting, bending, welding and finishing.
Welding and Assembly
Useful when the prototype must represent a fabricated structure or a multi component assembly. Joint design, distortion and post weld finishing need consideration.
Metal Additive Manufacturing
Can produce selected complex geometries and internal channels that are difficult to machine. Build orientation, supports, post processing and inspection affect the result.
Secondary Operations
Drilling, tapping, grinding, polishing, passivation and other suitable operations can bring the prototype closer to its functional or cosmetic requirements.
Design Considerations for Stainless Steel Prototype Machining
Stainless steel can be more demanding to machine than many aluminum alloys. Some grades work harden during cutting, and poor chip evacuation or excessive tool rubbing can shorten tool life and affect surface quality.
Tool Access and Geometry
Deep pockets, narrow slots, internal corners and long reach features can require specialized tooling or multiple setups. Internal corner radii should suit available cutting tools where design flexibility exists.
Wall Thickness and Workholding
Thin walls and unsupported sections may distort under cutting forces or clamping pressure. Discuss workholding and machining sequence during design for manufacturability review.
Threads and Mating Features
Specify thread standards, fits, engagement length and critical mating dimensions. Where assemblies matter, identify the features that control alignment, sealing or movement.
Corrosion and Surface Condition
Machining contamination, roughness and finishing choices can influence corrosion performance. Where specified, passivation should follow an appropriate procedure for the grade and application.
Drawing and Datums
Identify functional datums, geometric tolerances and critical dimensions clearly. Avoid applying tight tolerances to every feature when only selected interfaces control function.
Prototype Versus Production
Determine whether the goal is visual evaluation, fit checks, functional testing or production process validation. The answer influences material condition, inspection and manufacturing method.
Stainless Steel Prototype Tolerances and Surface Finish
Achievable tolerances depend on the part’s size, geometry, grade, machining setup, workholding, measurement method and the specific features being controlled. Do not assume that one tolerance applies to every dimension on a prototype.
| Requirement | What to specify | What affects feasibility |
|---|---|---|
| Linear dimensions | Nominal dimensions and individual tolerances | Feature size, tool access, setup and thermal effects |
| Position and alignment | Datums and geometric tolerances where necessary | Setup repeatability, inspection strategy and feature relationships |
| Surface roughness | Required Ra value or a clearly defined finish | Tooling, cutting parameters, material condition and finishing operations |
| Threads and fits | Thread standard, class or fit requirement | Thread size, engagement, inspection method and mating component |
| Corrosion performance | Grade, exposure conditions and specified treatment | Material chemistry, contamination, surface condition and finishing process |
For preliminary planning, CNC machined dimensions may sometimes fall within approximately ±0.05 mm to ±0.10 mm. This is indicative only, not a guaranteed Manufyn capability or a universal manufacturing standard. Tighter tolerances may be possible on suitable features after engineering review and agreement with the supplier.
Common finishes include as machined, brushed, bead blasted and polished. Specify a surface roughness value when performance requires it. Cosmetic descriptions alone may not provide enough information for consistent acceptance.
Quality Inspection for Stainless Steel Prototype Parts
Inspection requirements should be agreed before manufacturing begins. A clear inspection plan reduces the risk of receiving parts that meet general dimensions but fail at a critical interface.
- Dimensional inspection: Calipers, micrometers, bore gauges or other suitable instruments for specified features.
- CMM inspection: Coordinate measurement for complex geometry, positional requirements and critical datum relationships where appropriate.
- Material verification: Material certificates or additional verification when required by the drawing, purchase order or application.
- First article inspection: Dimensional and documentation review of an initial part when agreed for the project.
- Visual and finish inspection: Check burrs, visible damage, surface condition, cleanliness and specified finish.
- Documentation: Define the inspection report format, traceability and acceptance criteria in the RFQ.
Manufyn can coordinate inspection requirements with qualified manufacturing suppliers and align documentation expectations with the customer’s purchase order. Specific inspection methods and reports must be confirmed for each project.
What Affects Stainless Steel Prototype Cost?
Prototype pricing depends on both the raw material and the work required to convert it into an inspected, usable component. A lower raw material price does not necessarily result in a lower finished part cost.
Material Grade and Size
Grade availability, stock form, material dimensions and machining allowance influence material cost and waste.
Geometry and Machining Time
Deep pockets, small tools, complex contours, multiple setups and demanding surface finishes can increase cycle time.
Tolerances and Inspection
Tight tolerances, geometric controls, specialized gauges, CMM inspection and detailed reports can add cost.
Quantity and Repeatability
Programming, setup and fixture costs are spread differently across a single prototype, a small batch and repeat orders.
Finishing and Secondary Work
Polishing, passivation, heat treatment, welding or other specified operations may require additional processing and handling.
Packaging and Shipping
Export packaging, shipment dimensions, weight, transport method, destination and delivery terms affect the landed cost.
To compare quotations accurately, ask suppliers to clarify material grade, quantity, unit price, any one time setup or tooling charges, inspection scope, finishing, lead time and shipping terms.
How Long Does Stainless Steel Prototyping Take?
Lead time depends on drawing complexity, material availability, supplier capacity, machining hours, outside processing, inspection and shipping. A simple turned part and a multi setup milled housing will have different manufacturing requirements.
Before confirming a delivery date, establish whether the quoted lead time covers manufacturing only or includes finishing, inspection, export packing and delivery to the US destination. International transit and customs clearance should be considered separately unless explicitly included in the quotation.
Applications of Stainless Steel Prototype Parts
Robotics and Automation
Mounts, shafts, brackets, precision interfaces and selected end effector components.
Medical Equipment
Selected device housings, fixtures and functional test components, subject to applicable cleanliness and regulatory requirements.
Industrial Equipment
Machine components, fluid handling parts, housings, fittings and test assemblies.
Food and Process Equipment
Selected product contact components and equipment prototypes where the grade, finish and hygiene requirements are suitable.
Automotive and Mobility
Mounting hardware, brackets, test fixtures and components for design or assembly validation.
Marine and Energy
Selected fittings, enclosures and components evaluated for defined environmental and mechanical requirements.
From Stainless Steel Prototype to Low Volume Production
A prototype program can progress into low volume manufacturing when the design, material, inspection requirements and production method have been validated. The transition should be planned rather than treated as an automatic continuation of prototype machining.
Review the CAD model, drawing, material and critical interfaces.
Manufacture parts using an agreed process and acceptance criteria.
Evaluate fit, function, mechanical behavior and intended performance.
Incorporate changes and approve the revised specification.
Confirm repeatability, capacity, inspection and commercial terms.
Depending on the design, the production route may remain CNC machining or shift to fabrication, casting or another suitable process. Manufyn can coordinate supplier evaluation and procurement as the project requirements evolve.
Why Work With Manufyn for Stainless Steel Prototypes?
For US companies evaluating overseas manufacturing, the challenge is not only finding a supplier. It is aligning the drawing, material specification, quotation, inspection plan, delivery requirements and commercial expectations across the entire order.
Supplier Identification
Identify potential Indian manufacturing suppliers based on the component, process and project requirements.
Technical and RFQ Coordination
Coordinate drawing clarifications, DFM feedback, quotation comparisons and manufacturing questions.
Quality Coordination
Align inspection expectations, documentation requirements and issue follow up with the selected supplier.
Production Follow Up
Coordinate milestones and communicate progress, open questions and delivery risks.
Procurement Support
Compare commercial offers against scope, quantity, lead time, inspection and delivery terms.
Export Coordination
Coordinate packaging, shipping documentation and logistics arrangements for international deliveries.
Manufyn operates as a procurement and engineering coordination partner connecting international buyers with Indian manufacturing suppliers. Supplier selection, process feasibility, certification, inspection scope and delivery commitments are assessed against the specific project.
How to Request a Stainless Steel Prototype Quote
A complete RFQ helps suppliers assess manufacturing feasibility and prepare comparable quotations. Send the following information wherever available.
- 3D CAD model, preferably STEP or another agreed neutral format.
- 2D engineering drawing with units, dimensions, datums and tolerances.
- Required stainless steel grade and material condition.
- Prototype quantity and anticipated repeat or production volumes.
- Surface finish, polishing, passivation or other secondary operations.
- Critical dimensions, fit requirements and inspection expectations.
- Material certificates, traceability or additional documentation requirements.
- Required delivery date and destination ZIP code in the USA.
- Preferred shipping terms or any packaging requirements.
Share the application, operating environment and CAD model. The material and manufacturing route can then be reviewed before the quotation is finalized.
Send Your Prototype RFQ →Frequently Asked Questions
1. Which stainless steel is best for prototypes?
304 is a common general purpose option, 316 is often considered for more demanding corrosion environments, 303 is useful for many machining intensive parts, and 17-4 PH suits selected high strength applications. The best choice depends on the actual operating conditions and required properties.
2. Is stainless steel suitable for functional prototypes?
Yes. Stainless steel is useful when a prototype must evaluate strength, corrosion behavior, fit, wear or other properties relevant to the intended application. The chosen grade and material condition should represent the intended use.
3. Is CNC machining suitable for stainless steel prototypes?
Yes. CNC milling and turning are widely applicable to stainless steel prototypes, including housings, brackets, shafts, fittings and precision components. Geometry, tooling access, workholding and the selected grade affect feasibility and cost.
4. What tolerances can stainless steel prototype machining achieve?
Tolerances depend on part size, geometry, process, setup and inspection method. Some CNC machined features may achieve approximately ±0.05 mm to ±0.10 mm, but tighter or looser limits may apply. Critical dimensions should be reviewed and agreed before production.
5. How much do stainless steel prototype parts cost?
Cost depends on grade, material size, machining time, geometry, tolerances, quantity, finishing, inspection and shipping. A CAD file, drawing and quantity are the best starting point for obtaining a project specific quote.
6. Can US companies order stainless steel prototypes from India?
Yes. US companies can procure prototype parts from Indian manufacturers. The RFQ should define specifications, acceptance criteria, delivery terms and documentation. Export packaging, transit time, customs and landed cost should be considered when comparing offers.
7. What files are needed for a stainless steel prototype RFQ?
A 3D CAD model and dimensioned 2D drawing are preferred. Include material grade, quantity, tolerances, surface finish, inspection requirements and delivery destination. If a full drawing is not available, provide the best available model and explain the outstanding requirements.
8. Can stainless steel prototypes transition to low volume production?
Yes. After design validation, the part can move into low volume production if the process, supplier capacity, material specification, quality controls and commercial terms are suitable. The manufacturing route may remain the same or change to better suit the production quantity.
Need Stainless Steel Prototype Parts for Your Next Project?
Share your CAD model, drawing and quantity requirements with Manufyn. We can coordinate manufacturing feasibility, supplier quotations, inspection requirements and export logistics through our Indian manufacturing network.
Request a Stainless Steel Prototype Quote →For US engineering teams, provide your destination ZIP code and required delivery date so shipping can be considered in the quotation.